Small Fastener SKU Management Without Manual Spreadsheets
Small fastener SKU management becomes difficult when thousands of bolts, screws, nuts and washers are spread across a central warehouse, line-side bins and maintenance areas. A spreadsheet may list every part, yet still leave a supervisor unsure which specification is in a particular bin, how much usable stock remains or who is responsible for its next refill. Adding more rows does not solve a process in which physical movements are recorded late or described differently by each team.
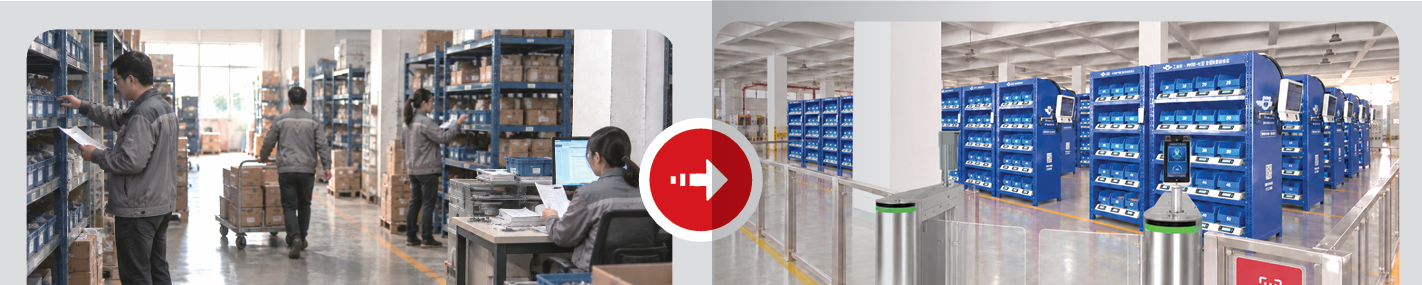
The practical goal is to give each approved SKU a consistent identity, each stock location a clear role and each important movement a defined record. Then the business can decide which items need connected bins, which can remain on conventional shelves and which require tighter access. This approach lets manufacturers improve visibility in stages without trying to place an entire material master inside one cabinet.
Quick Answer
Start by cleaning the fastener material master and identifying the SKUs that move most often or cause the most exceptions. Assign unique locations, standardize units of measure and define how receipts, transfers, issues, returns and corrections are recorded. Place a manageable group of high-frequency items in connected point-of-use storage where that supports the workflow. Keep the broader inventory system as the agreed source of record, and confirm any data exchange between systems for the actual project.
Key Takeaways
- Thousands of SKUs require a consistent data and location structure, not thousands of smart bins.
- A part number is only useful when its specification, unit of measure and approved equivalents are clear.
- Separate stock held in the warehouse from working stock available at the production line.
- Capture the few material movements that change availability or responsibility.
- Use connected storage for selected workflows, then expand according to measured needs.
Contents
- Why spreadsheets lose track of fasteners
- Build a reliable material master
- Prioritize the right SKUs
- Give every location a defined purpose
- Record material movements consistently
- Turn stock information into replenishment
- Where smart bins and cabinets fit
- Plan data ownership and integration
- Move away from spreadsheets in stages
- Frequently asked questions
Why Do Manual Spreadsheets Struggle at Scale?
A spreadsheet can be a useful working list. It becomes unreliable as a live inventory record when several people edit it at different times and material moves faster than entries are made. A warehouse may issue a carton, a line supervisor may transfer half of it to another cell, and an operator may consume parts before either movement reaches the file. The number displayed is precise, but the underlying status is uncertain.
Different copies create another problem. Purchasing may track supplier descriptions, production may use drawing numbers, and the warehouse may shorten both into familiar names. Similar fasteners can then appear as duplicates or, worse, be combined under one vague description. When a specification changes, no one is sure which copy should be updated first.
Scale magnifies these gaps. A low-frequency item can remain untouched for months, while another SKU moves repeatedly during each shift. Treating both with the same counting and update routine consumes attention without improving the decisions that matter most. Fastener inventory software can help organize records, but only after the business agrees what each item and transaction means.
Build a Reliable Fastener Material Master
Use one approved identifier for each distinct fastener SKU. Its description should contain the attributes needed to distinguish it from nearby items: product type, applicable standard or drawing, diameter, thread pitch where relevant, length, material or property class, finish and unit of issue. The exact fields depend on the product. “M8 screw” is not a sufficient identity if several M8 screws are approved for different tasks.
Standardize units before transferring data between systems. A purchasing record in cartons, a warehouse balance in pieces and a line-side bin measured by weight need a documented conversion. State the package quantity and whether partial packs may be issued. A wrong conversion can make a stock balance look credible while creating an incorrect replenishment request.
Control duplicates and substitutions. Two supplier references may point to the same approved internal item, while two similar catalog descriptions may represent different grades or finishes. Keep supplier references as mapped data rather than creating a new internal SKU for every label variation. Allow an alternative only when it has been reviewed and approved for the application; purchasing convenience should not silently change the material used at the line.
Assign ownership of the master record. Someone must approve a new SKU, retire an obsolete one and resolve conflicting descriptions. A clear change process also tells the warehouse and production teams when labels, bin assignments and existing stock must be reviewed after a revision.
Which SKUs Should Be Managed More Closely?
Do not assume that every item needs the same storage or issue method. First separate frequently consumed C-parts from slow-moving materials and selected higher-value or controlled items. Use purchase and issue history where available, then check it against what operators actually take. Purchase frequency alone may reflect order pack sizes rather than point-of-use demand.
Prioritize items that are picked often, have caused a shortage, are frequently confused with another specification or require repeated manual checks. Consider the consequence of a wrong pick as well as the unit price. A low-cost fastener can be important to an assembly, while a restricted tool or selected maintenance component may require named-user access rather than an open bin.
| SKU group | Typical management need | Possible starting approach |
|---|---|---|
| High-frequency standard fasteners | Convenient picking and dependable replenishment. | Clearly assigned line-side bins; connected storage where visibility is needed. |
| Similar-looking specifications | Strong identification and separation. | Distinct locations, complete labels and checked refills. |
| Slow-moving spare parts | Findability and periodic status review. | Identified central storage with accurate location records. |
| Selected controlled materials | Permission rules and appropriate issue records. | Enclosed storage or another approved controlled process. |
This grouping is a working decision tool. Review it as production schedules, suppliers and material specifications change. A useful pilot usually starts with a limited set of active SKUs rather than the full catalog.
Give Every Stock Location a Defined Purpose
A total quantity is not the same as available stock at the point of use. Identify the central reserve, each line-side working location and any maintenance or supplier-managed location separately. Record the location code on the physical storage point and in the inventory record. If a carton leaves the warehouse for a cabinet, the system should reflect that transfer according to the agreed transaction rules.
Keep one approved SKU identity per assigned bin unless a different arrangement has been explicitly designed and controlled. Similar-looking bolts should not share an unpartitioned container. The bin label should match the material master and remain readable during normal picking and refilling. If lot or batch information is required, determine how it is preserved when packages are opened or stock is combined.
A location structure also needs an exception state. Material with unclear identity, suspected mixing or a receipt discrepancy should not be shown as freely available production stock. Define a quarantine location and the person who can release or dispose of that material. A system may show a quantity, but the team must know whether it can actually be used.
Location design should follow material flow. Placing high-frequency parts near operators can simplify collection, provided the refill team can reach the point and maintain it. Broader smart warehouse planning should consider the route between reserve stock, working stock and the people who act on shortage signals.
Record the Movements That Matter
A replacement for manual spreadsheets should make important transactions clear without forcing operators through unnecessary steps for every small part. Define the events that change quantity, location, ownership or usability. Then decide which can be captured by connected equipment, which need a user action and which require review before posting.
| Movement | Question the record should answer | Control to define |
|---|---|---|
| Receipt | What approved SKU and quantity arrived? | Who verifies the package identity and accepted quantity? |
| Transfer | Which location supplied which destination? | When does stock become available at the receiving location? |
| Issue or consumption | What material left a working location? | Is a stock change enough, or is a user or job reference required? |
| Return | Is the material identified and suitable for reuse? | Who may return it to an approved bin? |
| Adjustment | Why does the recorded balance differ from physical stock? | Who investigates and authorizes the correction? |
Be precise about what a record proves. A detected decrease at a bin can support a material-use record; it may not, by itself, establish the individual who took the parts or the work order on which they were installed. Those details depend on the configured identification and issue workflow. Do not promise transaction-level traceability that the process does not collect.
Turn Inventory Information Into a Refill Decision
For each active SKU and location, define a level that prompts review before the stock needed during replenishment is exhausted. Consider consumption, the interval between reviews, internal transport, supplier time, package quantity and demand variation. The threshold should reflect how long it takes to restore usable material at that particular point, not a value copied from another site.
Assign an owner to every signal. A low-stock alert might call for a warehouse transfer, a buyer’s review or a supplier refill. State who receives it, who checks available reserve stock, who approves any purchase and who confirms that the bin was refilled. An alert left open after a physical refill can cause duplicate work; an alert closed before a refill can conceal a continuing shortage.
Vendor-managed or consignment workflows add commercial and data questions. Agree on stock ownership, supplier visibility, refill access, receipt confirmation and the event used for settlement. The NVMI vendor-managed inventory overview can inform the discussion, but the terms and process must be defined for the project.
Where Do Smart Bins and Cabinets Fit?
Connected cabinets are most useful when a physical picking point also needs accessible stock information. The NVMI-H open smart cabinet is designed for direct picking from weight-sensing units. Its connected platform supports review of stock changes, material-use records and low-stock alerts. It can be considered for high-frequency fasteners and suitable industrial consumables where open access fits the work.
For materials requiring configured user verification and permissions, the NVMI-D enclosed smart cabinet provides a different workflow. A mobile open cabinet may suit changing work areas, subject to placement, power and connectivity review. Select the storage type around users and material behavior; do not assign cabinet capacity simply by counting all entries in a spreadsheet.
A cabinet holds a chosen subset of working inventory. Thousands of catalog SKUs may remain in central storage, with selected fast-moving or controlled items distributed among appropriate points of use. Unit weight, bin size, pack format and expected pick quantity should be tested before using weight changes as a basis for quantity records. A sensor does not verify that a wrong part has been placed in the correct bin.
Decide Which System Owns Each Record
Before discussing an interface, draw the data flow. Which system creates and approves the SKU? Where is the authoritative stock balance for the warehouse? What happens when a cabinet detects a withdrawal, receives a refill or reports an adjustment? A clear mapping prevents two systems from treating the same movement as separate consumption events.
Specify the fields each exchange needs: item identifier, unit of measure, location, transaction type, quantity, timestamp and any required user, job or supplier reference. Define how a failed message is retried and how staff reconcile differences. A dashboard can show useful local information while an ERP or WMS remains the system of record; the relationship must be agreed rather than assumed.
ERP, MES, WMS and supplier-system interfaces should be reviewed against the actual platforms, available APIs and project scope. Start with the operational question the connection must answer. If the immediate problem is missed line-side refills, a reliable alert and confirmation process may be the first requirement. More detailed job-level consumption data can be assessed separately.
Move Away From Spreadsheets in Stages
Choose one representative area and a limited group of active SKUs. Clean their descriptions, confirm physical quantities and assign locations before importing records. Map the current path from receipt to use, including returns and stock corrections. The pilot should test a real replenishment cycle rather than only show that a dashboard displays a starting balance.
- Identify the approved item record and remove duplicate or ambiguous entries.
- Confirm units, package conversions, supplier references and any approved alternatives.
- Label central and point-of-use locations with consistent identifiers.
- Decide how each receipt, transfer, issue, return and adjustment is captured.
- Assign alert, refill and data-correction responsibilities across shifts.
- Test physical-to-system reconciliation and the response to an outage or uncertain bin.
- Review actual exceptions before adding more SKUs or locations.
Measure whether the new process answers questions the spreadsheet could not: Which locations are approaching a refill point? How many alerts remain unresolved? Where do repeated adjustments occur? Which SKUs are hard to find or frequently confused? Track the baseline and note changes in demand or staffing when interpreting the pilot. Expand only when the team can maintain the data and respond to exceptions consistently.
Frequently Asked Questions
Do we need one smart bin for every fastener SKU?
No. Prioritize the SKUs that benefit from point-of-use storage, frequent stock updates or access control. Slow-moving items may remain in identified central storage while sharing the same approved material master.
Can software fix inaccurate spreadsheet data automatically?
No. Duplicate items, wrong units and unclear locations must be resolved. Software can make new transactions easier to review, but importing unreliable starting records carries the same uncertainty into the new system.
How should we handle similar-looking fasteners?
Use complete descriptions, distinct assigned locations and a checked refill process. Where the consequence of a wrong pick is higher, define an additional verification step appropriate to the assembly or quality plan.
Does a cabinet stock change equal a confirmed production issue?
Not always. It shows movement at a connected location. Named-user, job or cost-center attribution requires those details to be captured in the configured workflow and mapped to the intended record.
Can suppliers see stock and refill cabinets?
That depends on the agreed vendor-managed arrangement, permissions and technical scope. Define data visibility, replenishment ownership, access and receipt confirmation before enabling a supplier workflow.
What is the best first group of SKUs for a pilot?
Choose a manageable set used frequently at one location, including items associated with shortages or repeated manual checks. Verify their specifications and units before setting thresholds and measuring the new process.
References & Sources
- Bear Bit NVMI-H, NVMI-D and NVMI-X product descriptions — current information on connected storage, stock records, replenishment alerts and model-specific access.
- GS1 standards guidance — general background on consistent identification of items and locations and the capture of movement data. This article does not claim a GS1-certified NVMI integration.
Plan a Manageable First Deployment
Share your top high-frequency SKUs, material categories, current spreadsheet and storage structure, issue process, user count and line-side replenishment workflow. Include stockout frequency, any shrinkage or specification-mixing problems, deployment locations, access-control needs, integration scope and target KPIs. The NVMI team can use those details to review the first suitable group of materials, bin arrangement and data workflow with you.